Turnkey Cold Extrusion (Cold Forging) + Multi-Axis CNC Precision Machining for Automotive ADAS, Surround-View (AVM), and Autonomous Driving Camera Upper & Lower Enclosures — Manufactured from High-Purity 1050 / 1070 Aluminum with 220–230 W/m·K Thermal Conductivity, Magnetic Tumbling Deburring, and Automotive-Grade Anodizing.
- ✅ Superior Thermal Dissipation (
1050 / 1070Pure Aluminum vs. Die-Cast ADC12): High-resolution automotive CMOS image sensors and ISP chips generate intense heat in compact spaces. By cold-extruding 99.5%–99.7% pure aluminum (AA 1050 / AA 1070), we achieve a thermal conductivity of220–230 W/m·K—nearly 2.4× higher than standard ADC12 die-cast aluminum (96 W/m·K). - ✅ 100% Pore-Free Cold-Extruded Density for True Anodizing & IP69K Sealing: Unlike high-pressure die casting which suffers from subsurface gas porosity, multi-stage cold extrusion (cold forging) produces a wrought, zero-porosity grain structure that accepts uniform clear, silver, or black anodizing without dark spots or blisters, while ensuring 100% hermetic waterproof sealing.
- ✅ High-Precision CNC Post-Machining (
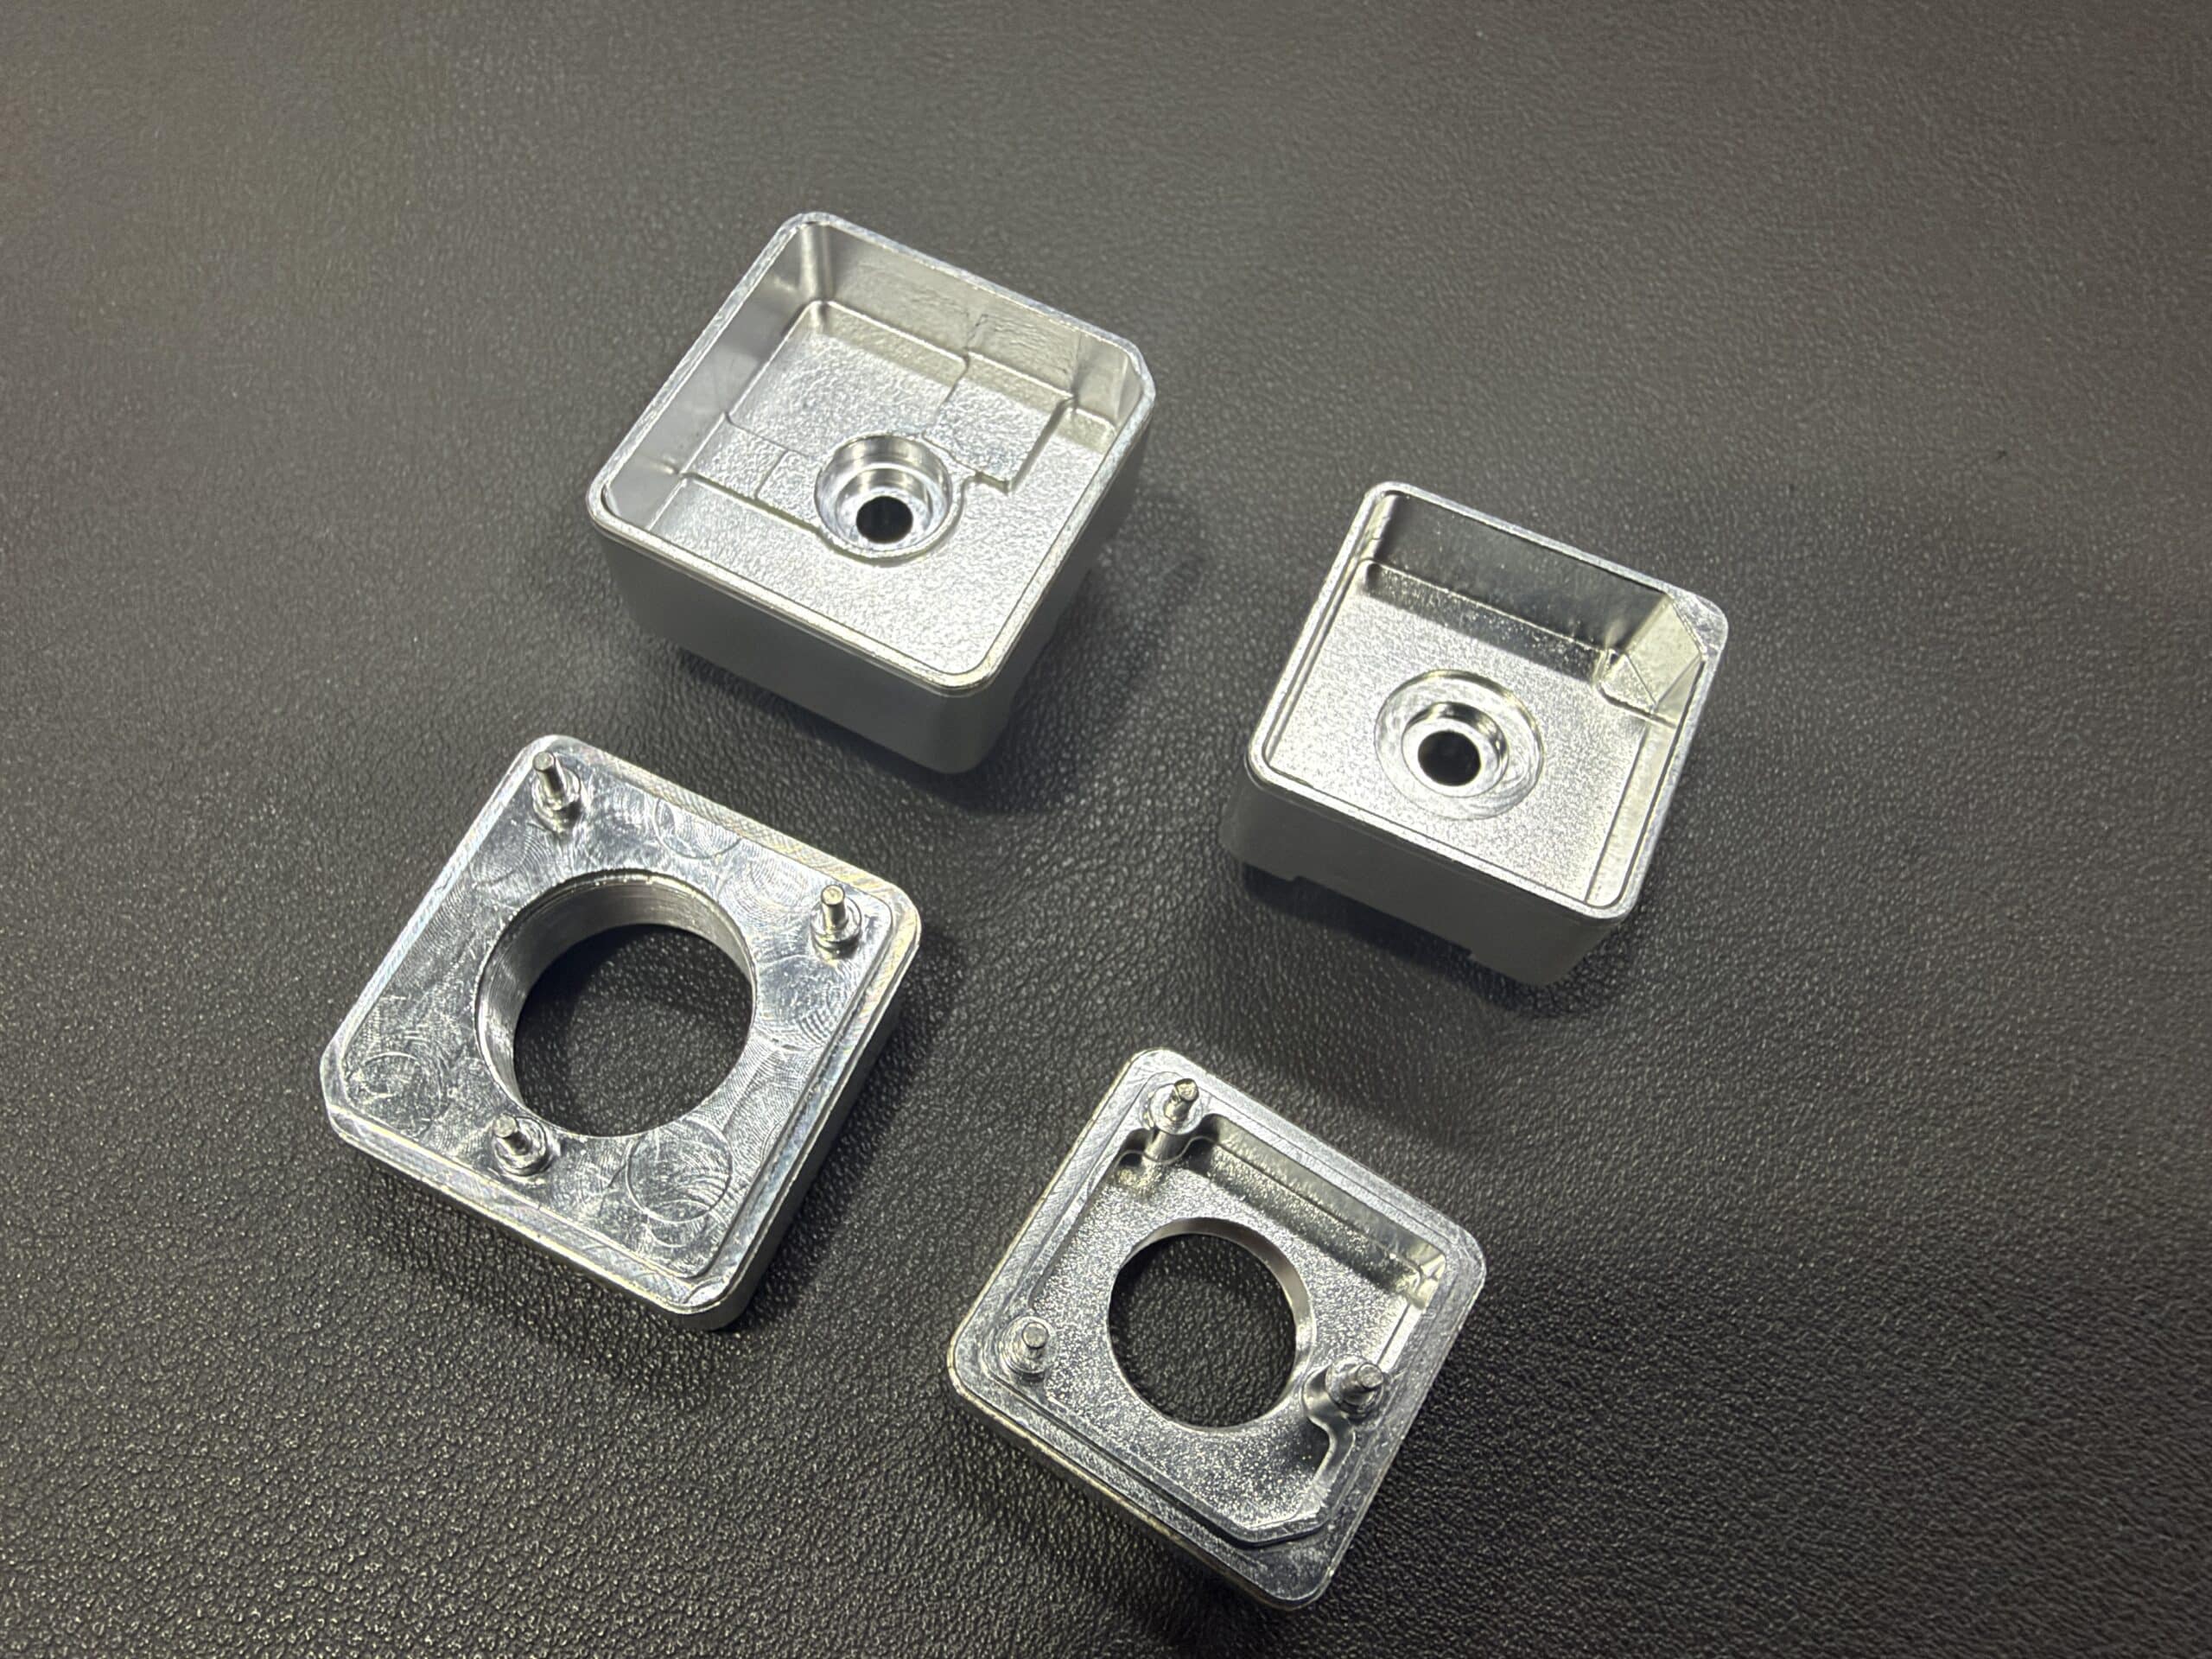
±0.01 mmOptical & Sealing Tolerances): While cold extrusion near-net forms the deep inner cavity, cylindrical FAKRA connector tube, anti-rotation tab, and internal PCB positioning pins in a single stroke, 4-axis CNC machining finishes the fine internal optical lens thread, interlocking upper/lower rabbet sealing step, and rear mounting datum pads. - ✅ Magnetic Tumbling Polishing (Zero Micro-Burrs on Internal Threads): Before anodizing, every housing undergoes automated magnetic pin tumbling polishing to eliminate microscopic CNC burrs inside the fine lens threads and internal corners—preventing particle contamination on sensitive camera CMOS sensors.
👉 Upload Your 2D/3D CAD Files (STEP, IGS, X_T, DWG, PDF) for a Free Cold-Extrusion + CNC DFM Review & 24-Hour Quote (100% Protected by Mutual NDA)
Visual Engineering Breakdown: Inside Our Cold-Extruded & CNC Machined Automotive Camera Housing


Technical Specifications: 1050 / 1070 Cold-Extruded & CNC Machined Camera Housing
| Engineering Parameter | Mindwell Production Specification (Verified Automotive Case) |
|---|---|
| Component Name & Application | Automotive ADAS / 360° Surround-View (AVM) / Rear-View Camera Upper & Lower Housing Set (Front Lens Shell + Rear Connector Shell) |
| Raw Material Grades | AA 1050 (Al 99.5%) / AA 1070 (Al 99.7%) High-Purity Wrought Aluminum Slug (Optional: AA 6061 / 6063 upon request) |
| Thermal Conductivity & Density | 222 – 234 W/(m·K) (Over 2.3× higher heat dissipation than ADC12 die-cast aluminum) | Density: 2.70 g/cm³ (100% Pore-Free) |
| Primary Forming Process | High-Tonnage Precision Cold Extrusion (Backward & Forward Cold Forging) — Near-net forming of deep square box cavity, cylindrical connector tube, anti-rotation tab, and internal PCB standoff pins in one press stroke |
| Secondary CNC Precision Machining | 4-Axis High-Speed CNC Turning & Milling: Fine Optical Lens Internal Thread (e.g., M12×0.5 / M14 / M16 Fine Pitch), Interlocking Waterproof Sealing Step, Rear Datum Pads, and Mounting Holes |
| Dimensional & Geometric Tolerances | Cold-Extruded Features: ±0.03 – ±0.05 mm | CNC Machined Lens Bore, Sealing Rabbet & Pin Spacing: ±0.01 mm | Lens-to-PCB Perpendicularity: ≤ 0.015 mm |
| Surface Finishing Protocol | 1. Magnetic Tumbling Polishing (Magnetic Pin Deburring) for 360° micro-burr removal + 2. Precision Anodizing (Clear / Natural Silver / Matte Black, 8–15 μm film thickness) or Chromate Passivation (SurTec 650 / TCP) |
| Ingress Protection & EMC Shielding | Designed for IP67 / IP6K9K Automotive Waterproof Sealing (Laser-welded, structural adhesive, or O-ring assembly) & 360° EMI/EMC Faraday Shielding |
| Cleanliness & Optical Quality Control | Ultrasonic Multi-Stage Hydrocarbon/DI-Water Cleaning, Go/No-Go Optical Thread Plug Gauging, 3D CMM Mating Step Inspection, Helium/Air-Decay Leak Testing, & Salt-Spray Corrosion Testing |
| Tooling Life & Lead Time | Cold Extrusion Carbide/HSS Dies: 300,000+ Strokes | Tooling + CNC Fixture Lead Time: 18–22 Days | Mass Production: 7–12 Days |
Why Leading Automotive Tier-1s Choose Cold Extrusion + CNC Over Die Casting or Full Bar-Stock CNC
1. 1050 / 1070 Cold Extrusion Solves the ADAS Camera Heat & Anodizing Bottleneck
Modern automotive ADAS and surround-view cameras pack high-wattage image sensors, SerDes chips, and power regulators inside an enclosure barely 25 × 25 mm in size. Traditional ADC12 aluminum die castings have low thermal conductivity (~96 W/m·K) and contain high silicon content (9.6–12% Si) plus internal micro-porosity—making decorative or uniform protective anodizing nearly impossible. By utilizing AA 1050 / 1070 pure aluminum cold extrusion, Mindwell delivers:
- 230 W/m·K Passive Cooling: Rapidly conducts heat away from the internal PCB through the housing walls without bulky external fins.
- Flawless Anodized Oxide Layer: Zero silicon smut and zero gas porosity allow a dense, uniform anodized film that passes strict automotive salt-spray and thermal-cycling standards.
- Laser-Weldable Purity: Unlike die-cast aluminum which outgasses and splatters during laser welding, pure 1050/1070 cold-forged shells can be hermetically laser-welded or bonded with zero weld blowholes.
2. Near-Net Cold Forging + Selective CNC Finishing Saves 55% Cost vs. Full Billet Machining
Machining a deep thin-walled camera housing with an external cylindrical FAKRA connector tube, an anti-rotation key tab, and three tiny internal PCB alignment pins (`Photo #1 & #3`) directly from solid aluminum bar stock requires 5-axis indexing and wastes over 75% of the material as chips. Our hybrid Cold Extrusion + CNC process forms the complex inner/outer 3D geometry and integral pins in a single 2-second cold-forging press stroke—leaving only the precision lens threads, sealing steps, and datum faces for fast high-speed CNC finishing.
3. Magnetic Tumbling Polishing + Ultrasonic Cleaning for Zero Sensor Contamination
Even a single microscopic metal burr falling onto a camera CMOS sensor causes a permanent dead-pixel defect. Mindwell subjects all CNC-machined camera shells to automated magnetic pin tumbling polishing (Magnetic Deburring): millions of stainless-steel micro-pins driven by a rotating magnetic field penetrate deep into the fine internal lens threads, corner thru-holes, and connector bores—polishing away every micro-burr and producing a uniform satin metallic sheen prior to final anodizing.
Frequently Asked Questions (FAQ)
Q1: What is the difference between AA 1050 and AA 1070 aluminum for cold-extruded camera housings?
A: Both are high-purity wrought aluminum alloys ideal for cold extrusion. AA 1070 (99.7% Al) offers slightly higher plasticity and thermal conductivity (~234 W/m·K) for ultra-deep backward/forward extruded tubes (like the rear FAKRA connector boss), whereas AA 1050 (99.5% Al) provides slightly higher baseline mechanical strength at an economical cost. Mindwell supports both grades according to your thermal and mechanical drawing specs.
Q2: How do you guarantee coaxiality and perpendicularity between the front lens thread and the internal PCB alignment pins?
A: In our secondary CNC machining stage, the cold-extruded shell is clamped in a precision pneumatic fixture referencing the internal PCB datum plane. The mating rabbet step, optical lens bore, and fine internal thread are finish-machined in a single clamping setup—holding lens-to-PCB perpendicularity within ≤ 0.015 mm and mating step clearance within ±0.01 mm.
Q3: Can the upper and lower shells be laser-welded after anodizing, or how is the sealing surface handled?
A: Yes. Depending on your assembly method (structural adhesive dispensing, O-ring screw fastening, or perimeter laser welding), we can either CNC-machine the interlocking sealing step after magnetic polishing/anodizing to expose fresh bare aluminum on the mating seam (as shown in Photos #1 & #4), or apply selective masking during anodizing.
Request a Free Cold-Extrusion + CNC DFM Review & 24-Hour Quote
Looking for a reliable manufacturer for custom Automotive Camera Housings, LiDAR/Radar Enclosures, or Cold-Forged Aluminum Heat Sinks? Send your 2D/3D CAD files to Xiamen Mindwell Precision Manufacture Co, Ltd. for an itemized tooling and unit price quote within 24 hours.
- 📧 Engineering RFQ Email: service@mnwell.com | Online RFQ Form
- 📎 Supported Formats:
STEP (.stp),IGES (.igs),X_T,DWG,PDF - 🔒 100% IP Protection: Full Mutual NDA available prior to file transfer.